A Pharmaceutical company plays an important role in the healthcare system by supporting the development, manufacturing, quality management, marketing, and supply of medicines. In India, the pharmaceutical sector serves a wide range of healthcare needs and connects manufacturers, distributors, pharmacies, hospitals, healthcare professionals, and other organisations.
However, a pharmaceutical company is not defined by its product catalogue alone. Its operations may involve scientific research, product planning, regulatory documentation, manufacturing partnerships, quality assurance, packaging, inventory management, and distribution.
For businesses looking for Pharmaceutical products or manufacturing services, understanding these activities can help them evaluate potential suppliers more carefully.
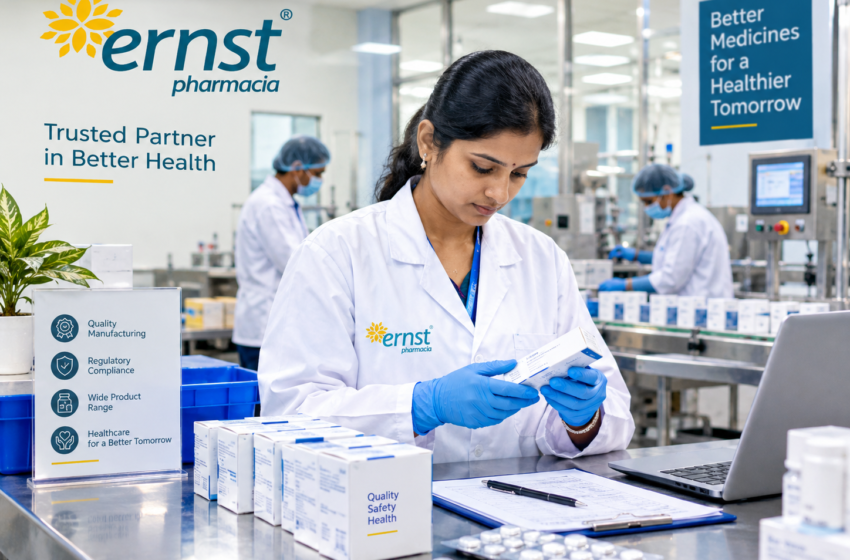
Ernst Pharmacia is an Indian pharmaceutical company whose official website lists a broad product portfolio and services that include third-party manufacturing. This article explains how pharmaceutical companies operate, what quality-related factors matter, and how businesses can assess a pharmaceutical company before entering into a commercial relationship.
1. What Is a Pharmaceutical Company?
A Pharmaceutical company is an organisation involved in one or more activities related to medicines and pharmaceutical products. Depending on its business model, it may develop products, manufacture medicines, arrange contract manufacturing, distribute products, or market pharmaceutical brands.
Not every pharmaceutical company performs every activity itself. Some operate their own manufacturing facilities, while others work with external manufacturers under defined commercial and regulatory arrangements.
Common types of pharmaceutical businesses include:
Pharmaceutical research and development companies
These organisations focus on discovering new drug candidates, developing formulations, conducting studies, and generating scientific data. Research and development activities depend on the product, development stage, and applicable regulatory requirements.
Pharmaceutical manufacturing companies
These Pharmaceutical manufacturing companies medicines using appropriate facilities, equipment, personnel, and quality systems. Their authorised activities depend on their manufacturing licences and the products they are permitted to produce.
Pharmaceutical marketing companies
These businesses focus on product portfolios, branding, market development, customer relationships, and distribution arrangements. Depending on their role, they may work with licensed manufacturers to produce products under an agreed brand or commercial arrangement.
Third-party pharmaceutical manufacturing companies
These manufacturers produce products for other businesses under agreed specifications and responsibilities. This model can allow a business to access manufacturing capabilities without establishing its own factory.
Pharmaceutical distribution companies
Distributors manage the movement and supply of medicines through the pharmaceutical supply chain. Their responsibilities may include procurement, inventory management, appropriate storage, order fulfilment, and distribution in accordance with applicable requirements.
Some organisations combine several of these business models.
2. Why Is the Pharmaceutical Industry Important in India?
India has a significant pharmaceutical manufacturing and supply sector that serves domestic and international markets. Pharmaceutical businesses support access to a wide range of medicines and contribute to manufacturing, distribution, research, technical employment, and healthcare-related services.
The industry includes companies of different sizes, from specialised manufacturers to organisations with broad product portfolios.
Its importance can be understood through several areas.
Access to medicines
Pharmaceutical companies help make different types of medicines available through authorised supply channels. Availability depends on product approvals, manufacturing capacity, demand, and distribution arrangements.
Manufacturing capabilities
The sector includes facilities that manufacture different dosage forms, such as tablets, capsules, oral liquids, topical preparations, and specialised products where suitable facilities and approvals exist.
Product development
Formulation development and process improvement can help pharmaceutical businesses address technical requirements, product stability, manufacturing consistency, and changing market needs.
Employment and technical expertise
The industry requires professionals in production, quality control, quality assurance, regulatory affairs, research, engineering, warehousing, sales, and distribution.
Domestic and international supply
Pharmaceutical companies may serve local markets, distribute products across India, or export to international markets. Export activity requires compliance with the applicable requirements of the destination market as well as relevant Indian requirements.
3. How Does a Pharmaceutical Company Work?
The operating process differs by company and product, but a pharmaceutical business may manage the following stages.
Step 1: Product planning
The company identifies a product requirement based on its business strategy, available capabilities, healthcare needs, market research, and applicable regulations.
The proposed product must be assessed for technical feasibility and the regulatory requirements relevant to its intended use and market.
Step 2: Product development or selection
Depending on the business model, the company may develop a formulation, select an existing authorised product, or evaluate a product for contract manufacturing.
The composition, strength, dosage form, specifications, packaging, and required documentation must be established appropriately.
Step 3: Manufacturing arrangements
The company determines whether the product will be manufactured at its own authorised facility or through a qualified external manufacturing partner.
When manufacturing is outsourced, responsibilities should be defined clearly. A commercial agreement does not remove the need to comply with applicable regulatory requirements.
Step 4: Quality control and quality assurance
Quality control includes relevant sampling, testing, and assessment against established specifications. Quality assurance oversees the broader systems and procedures used to maintain quality.
Depending on the product, controls may cover raw materials, in-process checks, finished-product testing, packaging, documentation, and batch review.
Step 5: Packaging and labelling
Medicines require packaging suitable for the product and its intended storage conditions. Labels must meet applicable requirements and accurately identify the product and its relevant details.
Packaging and labelling controls help reduce errors and support product traceability.
Step 6: Storage and distribution
After the required approvals and release procedures, products are stored and distributed under suitable conditions. Some products require specific temperature or handling controls.
Step 7: Customer support and post-market responsibilities
Pharmaceutical companies may need procedures for receiving product complaints, investigating quality concerns, maintaining records, and managing recalls or other corrective actions where necessary.
The specific responsibilities depend on the company’s role, the product, contractual arrangements, and applicable law.
4. Understanding Pharmaceutical Product Categories
Pharmaceutical companies may organise their products by therapeutic area or dosage form. A therapeutic category groups products according to the area of healthcare they relate to, while a dosage form describes how a medicine is prepared for administration.
Common therapeutic categories
Examples include:
- Cardiology
- Gynaecology and women’s healthcare
- Dermatology
- Orthopaedics
- Neurology
- Gastroenterology
- Diabetic care
- Respiratory care
- Ophthalmology
- Oncology
- Hepatology
- Nephrology and urology
- Antibiotics and antivirals
- Nutritional supplements and nutraceuticals
The presence of a category in a company’s portfolio does not mean every product within that category is available or authorised for every market. Product-specific verification remains important.
Common pharmaceutical dosage forms
| Dosage form | General description |
|---|---|
| Tablets | Solid preparations containing measured quantities of ingredients |
| Capsules | Preparations enclosed in a suitable capsule shell |
| Syrups and oral liquids | Liquid formulations intended for oral administration |
| Oral suspensions | Liquid preparations in which ingredients are dispersed |
| Ointments and creams | Semisolid preparations commonly used on the skin |
| Eye or ear drops | Liquid preparations designed for the relevant application |
| Injectables | Preparations intended for administration by injection and subject to applicable requirements |
| Soft gelatin capsules | Capsules with a soft shell suitable for specific formulations |
| Respules and inhalation products | Products designed for specific inhalation-related delivery systems |
Each dosage form has its own formulation, manufacturing, packaging, and quality considerations. The appropriate requirements depend on the product.
5. Why Quality Matters in the Pharmaceutical Industry
Medicine quality is a central consideration because products must meet their established specifications and applicable requirements throughout their lifecycle.
Quality cannot be established by looking at the packaging or relying on a general marketing statement. It depends on suitable materials, controlled processes, appropriate testing, accurate documentation, and effective quality systems.
Raw material controls
Materials should be assessed according to approved specifications and procedures before they are used in manufacturing.
Manufacturing controls
Production processes should be performed according to approved procedures, with relevant parameters monitored and documented.
Laboratory testing
Tests are selected according to the product, its specifications, and applicable requirements. Different dosage forms require different testing programmes.
Documentation and traceability
Manufacturing and quality records help establish what happened during production and testing. They also support investigations and product traceability.
Batch review and release
A batch should undergo the required review and authorised release process before it is distributed. A single passing test does not replace the review of other relevant records and requirements.
Storage and transport
Products should be stored and transported under suitable conditions to protect their quality. Requirements vary according to the medicine and its packaging.
6. What Are GMP and Pharmaceutical Quality Standards?
Good Manufacturing Practices (GMP) are requirements and systems intended to ensure that pharmaceutical products are consistently manufactured and controlled to the required quality standards.
In India, relevant requirements include provisions of the Drugs and Cosmetics Rules, 1945, including Schedule M. The applicable requirements depend on the facility, activity, product, and current regulatory position.
GMP-related controls may address:
- Premises and equipment.
- Personnel and training.
- Sanitation and hygiene.
- Production procedures.
- Quality control.
- Documentation and record management.
- Equipment maintenance and calibration.
- Validation and other process controls where applicable.
- Handling of deviations and complaints.
- Product recall procedures where required.
Businesses evaluating a pharmaceutical manufacturer should verify relevant licences, facility details, certificates, and product-specific documentation. A general claim of certification should not be treated as proof that every product or activity is covered.
7. Pharmaceutical Manufacturing: Own Facilities and Third-Party Models
Pharmaceutical companies may use different manufacturing models depending on their resources, capabilities, product requirements, and business objectives.
Own manufacturing facilities
A company operating its own manufacturing facility is responsible for the applicable infrastructure, staffing, production operations, quality systems, and regulatory obligations.
The facility must have the required authorisations for the manufacturing activities it performs.
Third-party manufacturing
Under a third-party manufacturing arrangement, a company engages an external manufacturer to produce specified products under agreed conditions.
Potential considerations include:
- Manufacturing-site suitability.
- Product and formulation requirements.
- Required licences and permissions.
- Quality responsibilities.
- Packaging and labelling.
- Minimum order quantities.
- Testing and batch documentation.
- Production planning and delivery.
- Commercial terms and complaint handling.
Third-party manufacturing can reduce the need for a business to establish every part of its own manufacturing infrastructure. However, it does not remove the need to verify quality, regulatory responsibilities, and the suitability of the arrangement.
8. How to Evaluate a Pharmaceutical Company
Businesses looking for a pharmaceutical supplier or manufacturing partner should consider more than price and the number of products listed online.
Review the product portfolio
Check whether the company offers the required products, strengths, dosage forms, and packaging options. Confirm availability and the applicable product permissions.
Verify relevant licences and documents
Request the documentation applicable to the specific product and activity. Verify the manufacturing facility and relevant authorisations.
Assess quality arrangements
Ask about quality-control procedures, batch records, testing documentation, complaint handling, and the responsibilities of the parties involved.
Understand manufacturing capabilities
If production is outsourced, confirm the identity of the proposed manufacturing facility and whether its capabilities and authorisations suit the product.
Check supply planning
Discuss estimated production schedules, order quantities, material availability, storage requirements, and dispatch arrangements.
Review commercial terms
Confirm pricing, taxes, packaging costs, minimum order quantities, payment terms, and any additional charges in writing.
Evaluate communication and support
Clear communication helps businesses coordinate product requirements, documentation, orders, and quality-related concerns.
No single factor establishes that a company is the right choice. Evaluation should reflect the specific product, market, and business requirement.
9. The Role of Technology in Modern Pharmaceutical Companies
Technology can help pharmaceutical organisations improve traceability, document management, inventory visibility, and coordination between departments.
Examples include:
Electronic documentation
Digital systems can help manage approved procedures, training records, batch documentation, and document revisions when appropriately implemented and controlled.
Inventory management
Inventory systems can support stock monitoring, expiry-date tracking, demand planning, and appropriate stock rotation.
Manufacturing data
Suitable manufacturing systems can record process information and support the review of production performance.
Supply-chain visibility
Digital tracking tools can help businesses monitor orders, shipments, and stock movement.
Data integrity
Electronic systems must be managed with suitable access controls, review procedures, backups, and other safeguards appropriate to their intended use and applicable requirements.
Technology supports quality and efficiency, but it does not replace qualified personnel, sound procedures, or regulatory compliance.
10. Ernst Pharmacia: Pharmaceutical Products and Business Services
Ernst Pharmacia is an Indian pharmaceutical company based in Panchkula, Haryana. Its official website presents a broad product portfolio across multiple therapeutic categories and lists third-party manufacturing among its business services.
The company website includes categories such as cardiology, gynaecology, dermatology, neurology, respiratory care, oncology, orthopaedics, gastroenterology, and other pharmaceutical segments.
For businesses considering its products or services, the relevant next step is to discuss the specific requirement directly with the company.
Product portfolio and availability
Businesses should identify the required product, strength, dosage form, pack size, and quantity. Current availability and applicable product documentation should be confirmed for the specific item.
Third-party manufacturing enquiries
Businesses interested in contract manufacturing should discuss manufacturing feasibility, the proposed facility, product specifications, minimum order quantities, packaging, quality documentation, production estimates, and commercial terms.
Quality and regulatory verification
Before placing an order, request the documents relevant to the product and manufacturing arrangement. Verify applicable licences, permissions, facility details, and quality records.
Business communication
Clear communication helps both parties understand requirements, timelines, documentation, and responsibilities before confirming an order.
To learn more about the company’s published services, visit the official website:
- Website: https://ernstpharmacia.com/
- Contact page: https://ernstpharmacia.com/contact-us/
- Third-party manufacturing information: https://ernstpharmacia.com/pharmaceutical-third-party-manufacturing-india/
11. The Future of the Pharmaceutical Industry in India
The pharmaceutical industry continues to adapt to changing healthcare requirements, technology, regulation, and supply-chain expectations.
Several areas are important for its continued development.
Quality-focused manufacturing
Companies need systems that support consistent production, reliable documentation, appropriate testing, and effective handling of quality issues.
Research and formulation development
Scientific and technical capabilities can help businesses evaluate new formulations, improve processes, and address product-specific challenges.
Digital transformation
Digital tools can support documentation, inventory management, data review, and supply-chain coordination when implemented appropriately.
Responsible distribution
Reliable storage, handling, traceability, and distribution practices help protect product quality as medicines move through the supply chain.
Regulatory awareness
Pharmaceutical companies must monitor applicable requirements and ensure that their products and activities meet the relevant obligations.
Strong business relationships
Transparent communication and clearly documented responsibilities can help manufacturers, suppliers, distributors, and other businesses work together more effectively.
The future of the sector depends not only on market expansion but also on quality systems, technical capability, responsible business practices, and compliance.
Frequently Asked Questions
1. What does a pharmaceutical company do?
A Pharmaceutical company may develop, manufacture, market, or distribute medicines. Its responsibilities depend on its business model, licences, product portfolio, and role in the supply chain.
2. What is the difference between a pharmaceutical company and a pharmaceutical manufacturer?
A Pharmaceutical manufacturer produces medicines at an authorised facility. A pharmaceutical company may manufacture products itself or engage external manufacturers, depending on its business model and regulatory responsibilities.
3. What is third-party pharmaceutical manufacturing?
It is an arrangement in which a business engages an external manufacturer to produce pharmaceutical products under agreed specifications, quality requirements, and commercial terms.
4. What are GMP standards in pharmaceutical manufacturing?
GMP standards for Good Manufacturing Practices are systems and requirements intended to ensure that medicines are consistently manufactured and controlled according to the required quality standards.
5. What should I check before choosing a pharmaceutical company?
Review the relevant Product portfolio, licences, manufacturing arrangements, quality documentation, supply capabilities, commercial terms, and responsibilities that apply to your particular requirement.
6. Does Ernst Pharmacia offer third-party manufacturing?
Ernst Pharmacia lists third-party manufacturing among the services on its official website. Specific product requirements, manufacturing arrangements, documentation, and commercial terms should be confirmed directly.
7. Which pharmaceutical dosage forms are commonly available?
Common dosage forms include tablets, capsules, syrups, oral suspensions, creams, ointments, drops, and selected specialised formulations. Availability depends on the company and the relevant manufacturing capabilities and authorisations.
8. Why is pharmaceutical quality control important?
Pharmaceutical Quality control helps determine whether materials and medicines meet established specifications. It works alongside quality assurance, manufacturing controls, documentation, and authorised batch-release procedures.
9. Can a pharmaceutical company outsource manufacturing?
A company may use a third-party manufacturing arrangement where permitted and appropriate. The relevant parties must comply with applicable regulatory requirements and clearly define their responsibilities.
10. How can I contact Ernst Pharmacia?
You can visit ernstpharmacia.com/contact-us/ to review the company’s current contact information and submit a business enquiry.
Conclusion
A Pharmaceutical company in India contributes to the healthcare supply chain through activities such as product planning, manufacturing, quality management, packaging, and distribution. The exact responsibilities depend on its business model and the products it handles.
For businesses evaluating pharmaceutical suppliers or manufacturing services, the most important considerations include suitable product availability, verified documentation, appropriate quality systems, regulatory compliance, clear commercial terms, and reliable communication.
Ernst Pharmacia presents a broad pharmaceutical portfolio and third-party manufacturing services on its official website. Businesses interested in working with the company should discuss their specific requirements and verify the relevant product, manufacturing, quality, and regulatory documentation before proceeding.
Disclaimer: This article provides general information about the pharmaceutical industry and business operations. It is not medical advice, a regulatory approval, or a guarantee of any company’s product quality or compliance status. Verify current requirements and product-specific documentation with the relevant authorities and qualified professionals.